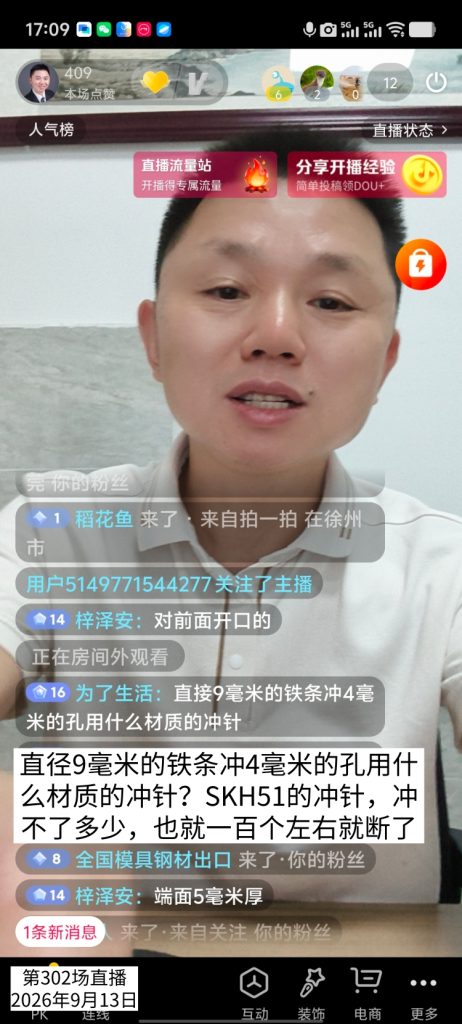
I. Problem Description: When punching a 4.0mm hole in a 9mm iron bar, an SKH51 punch breaks after just over 100 punches. What material should be used?
Question from a live stream viewer: When punching 4.0mm holes in a 9mm-diameter iron bar (round bar), I’m currently using SKH51 high-speed steel punches, but they don’t last long—the punches break after punching just over 100 products. What type of die steel should I switch to?
II. Analysis of Failure Causes: Why Does SKH51 Inevitably Break Under These Operating Conditions?
Conclusion: This is an extreme operating condition where “the punch diameter is smaller than the sheet thickness.” SKH51 is hard and brittle, making it a classic example of incorrect material selection.
1) Extremely Harsh Operating Conditions: Punching a 4.0 mm hole in a 9 mm round bar results in a punching ratio less than 1:1 (hole diameter < material thickness). During the punching process, the punch is subjected to extreme lateral forces and bending stresses, placing extremely high demands on the die steel’s resistance to chipping and the quality of its metallurgical properties.
2) SKH51 is inherently too brittle: SKH51 is a W6Mo5Cr4V2-series high-speed steel (containing approximately 6.0% tungsten). It can achieve a hardness of 62–64 HRC and offers excellent wear resistance, but it is highly brittle.
3) Microscopic cracks are the root cause of fracture: Conventional cast high-speed steel has limited metallurgical quality, and its microstructure contains a large number of microscopic cracks invisible to the naked eye. Under the high-stress, repetitive impact of punching small holes in thick sheets, these cracks propagate rapidly, leading to punch fracture. The fact that this user’s punch broke after punching more than 100 holes precisely confirms this failure mechanism.
III. Solution: Switch to 8566 crack-resistant steel
Recommended Solution: Use Yuhui Mold Steel’s proprietary 8566 chipping-resistant steel to manufacture the punches.
Key Performance Parameters of 8566 Chipping-Resistant Steel:
| Project | Parameter |
| Hardness | 58–60 HRC |
| Anti-cracking performance | 4 times that of high-speed steel SKH9, and 2 times that of D2 |
| Main application | Address the cracking issues that cannot be resolved with high-hardness mold steels such as D2, DC53, and SKH9. |
Typical applications: stainless steel stamping, sharp-corner stamping, and thick-plate stamping—especially under demanding conditions where the hole diameter is smaller than the plate thickness and the stamping ratio is less than 1:1.

Real-World Case Study: Mr. He from Hangzhou Successfully Punched a 4.5mm Hole in an 8mm Round Bar
Mr. He’s working conditions in Hangzhou closely resemble those in this case study—punching a 4.5mm hole in an 8mm round bar:
1) He tried Cr12MoV, H13, and DC53** in succession, but none of them worked; the punch would break after punching just a few products;
2) He was once forced to switch to manual drilling, which—with over 1 million holes drilled per year—was inefficient and costly, making automated punching unfeasible;
3) After switching to 8566 chipping-resistant steel punches, Mr. He reported: “It worked! We successfully punched 4.5mm holes in 8mm round bars using the 8566 punches.” If production is later converted to automated punching, the efficiency and cost advantages will be even more pronounced.
IV. Conclusion and Material Selection Recommendations
For applications where the punched hole diameter is smaller than the sheet thickness (ratio < 1:1), the core criterion for material selection is **crack resistance**, rather than simply pursuing high hardness:
1) SKH51: High hardness and good wear resistance, but highly brittle; combined with microcracks, it will break after more than 100 punches—incorrect material selection;
2) Cr12MoV / H13 / DC53: Conventional high-hardness die steels, none of which can withstand the stresses of such operating conditions;
3) 8566 crack-resistant steel: With a hardness of 58–60 HRC and crack resistance four times that of SKH9, it is a targeted solution for punching small holes in thick sheets.
This user is punching a 4.0-mm hole in a 9-mm iron bar using a punch made from 8566 anti-chipping steel, which is expected to replicate Mr. He’s successful case.
Using 8566 die steel for punch chipping—it’s like night and day compared to the old methods.
*************
Wu Dejian’s tool steel, the chief of staff of the user, bought everything he had used.